
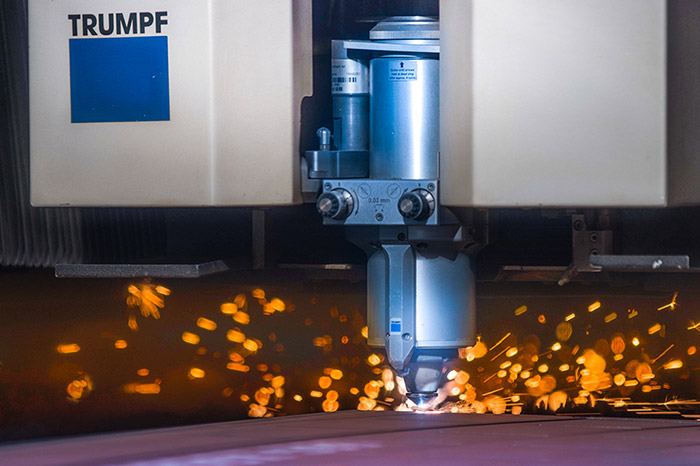
Aluminum offers low weight, excellent conductivity, and strong corrosion resistance, but high-speed cutting presents specific challenges. Heat can soften the material and produce gummy chips around the cutting zone.
Machine settings, tool geometry, lubrication, and chip control all influence results. For top-grade production, an experienced aluminium cutting service uses specific methods to manage heat effectively.
Why aluminum produces gummy chips
Aluminum contains properties that make chip control tricky during machining. Its softness and ductility allow chips to cling to the cutting edge instead of breaking cleanly. Friction adds more heat, which softens the material and encourages buildup around the tool. Sharp cutting edges, suitable rake angles, and polished tool surfaces help reduce adhesion.
Operators also select cutting speeds and feed rates that support smooth chip evacuation. Proper chip control keeps the cutting zone cleaner and reduces production interruptions. When operators match tool geometry with the specific aluminum grade, they gain better control over chip formation and achieve cleaner edges with less material buildup.
Controlling heat during aluminum cutting
Thermal buildup presents another major challenge during aluminum cutting. Excess heat softens the workpiece, increases tool friction, and may affect dimensional accuracy. Operators manage this issue through suitable spindle speeds, feed rates, coolant flow, and tool selection.
Lubrication reduces friction between the cutting edge and aluminum surface, while efficient chip removal helps move hot material away from the cutting zone. Air cooling also helps in applications where liquid coolant is unsuitable. Monitoring temperature and cutting behavior gives operators useful feedback during production.
Choosing suitable tools and settings
Tool selection directly affects aluminum cutting performance. Carbide tools with polished surfaces work well because they reduce friction and resist material adhesion. Operators also select flute designs that provide enough space for chips to exit the cutting area smoothly.
Excessive feed rates may increase heat and chip thickness, while very low feed rates may cause rubbing instead of efficient cutting. Manufacturers therefore match tool diameter, spindle speed, feed rate, and depth of cut with the aluminum grade and component design. Correct settings improve surface quality, reduce tool buildup, and support consistent production.
Improving cutting results
Reliable aluminum cutting comes from controlling several factors together. Operators inspect tool condition, monitor chip appearance, check cutting temperatures, and adjust machine settings when production conditions change. Clean workholding also helps maintain consistent positioning during each operation.
Regular tool inspection prevents worn edges from generating extra friction and heat. Advanced machines can use optimized cutting parameters for specific aluminum alloys and component sizes.